HAINING DULETAI NEW MATERIAL CO.,LTD

Duletai New Material

  • HOMEPAGE
  • NEWS
  • ABOUT US
  • SERVICES
  • PRODUCTS
    • DURAFLEX
    • DURATARPS
    • DURABLINDS
    • DURASCREEN
    • DURASUNTEX
    • DURAOXFORD
    • DURAECO
  • APPLICATIONS
  • CONTACT US
REQUESTFOR QUOTE

Category: Technology

PVC Surface Finishes & Anti-Wicking

  • 0
admin
Saturday, 17 October 2026 / Published in Technology
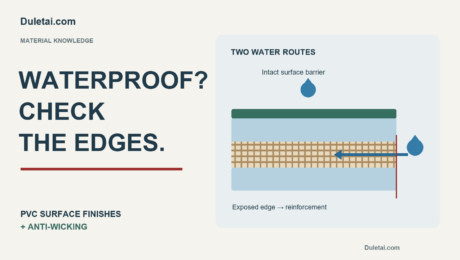
PVC fabric cross-section distinguishing the intact surface barrier from water movement along exposed reinforcement

Views: 144

DULETAI MATERIAL GUIDES · SURFACE AND STRUCTURE

Two PVC tarpaulins look equally waterproof. Why does one stay easier to clean, while another develops marks around its cut edges? And does choosing knife-coated fabric or a PVDF finish tell you how long it will last?

Start by separating the jobs of the surface finish, the PVC barrier and the polyester reinforcement. This guide connects those layers to anti-wicking, welding, physical-performance tests and a fair knife-coated versus laminated comparison.
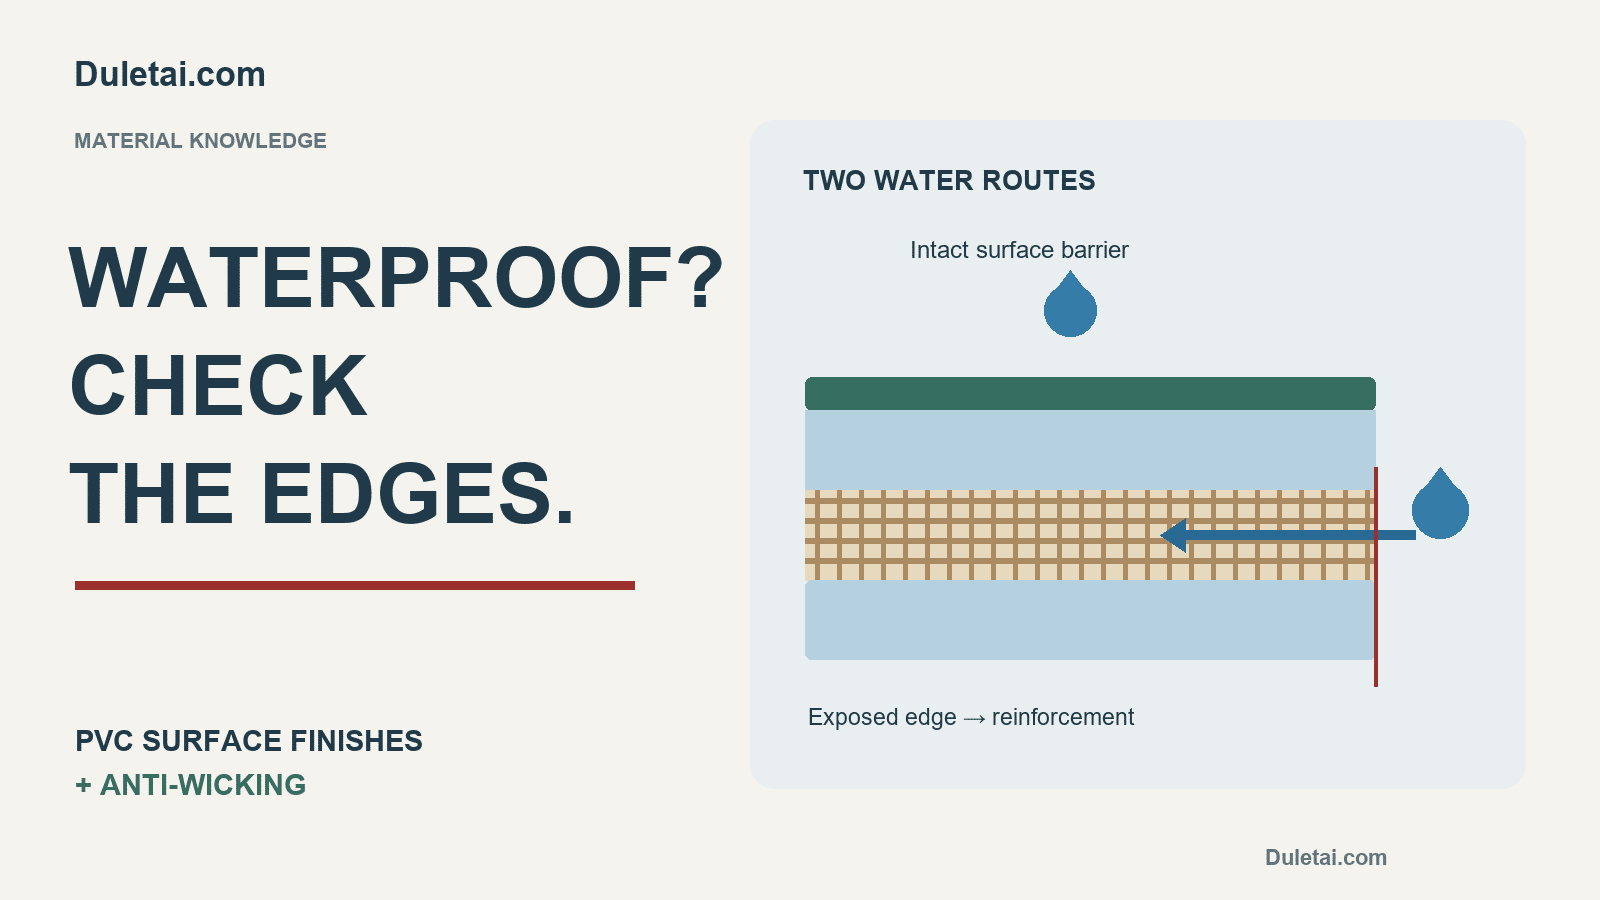
PVC fabric cross-section showing an intact surface barrier and a separate water route at exposed reinforcement
BUYER TAKEAWAY

Specify the construction, finish and exposure together. Surface waterproofing, reinforcement anti-wicking and seam watertightness need separate evidence. A finish-function reference period is not the lifespan or warranty of the whole fabric.

WATCH THE VIDEO

Watch our four-minute guide to acrylic and PVDF finishes, anti-wicking and the difference between surface protection and whole-fabric performance.

Watch on YouTube

EXPLORE THE MATERIAL

Open a topic to read its explanation. Long sections scroll inside the panel; select the heading again to close it.

01

Find the layers and the manufacturing route

A PVC tarpaulin is a composite. Duletai uses polyester filament yarns in the woven reinforcement. That fabric, the PVC layers and any specified surface finish contribute different properties. A glossy surface does not tell you the yarn construction, and a high finished weight does not identify how much reinforcement is inside.

Simplified PVC fabric layers: surface finish, PVC barrier and polyester reinforcementDIFFERENT LAYERS. DIFFERENT JOBS.Surface finish, if specifiedPVC water barrierPolyester filament fabricReverse-side PVCConceptual section; layer thicknesses are not to scale.
A simplified layer map. The finish is optional and the actual number of layers depends on the specified construction.
Part Main role What to specify
Woven reinforcement Provides the textile load-bearing network. Yarn, weave and direction affect mechanical behaviour. Polyester filament yarn specification, warp/weft construction and finished-material strength.
PVC layer or film Forms the main continuous barrier and contributes flexibility, handling and surface behaviour. Formulation, finished mass/thickness, exposure and required physical performance.
Bonding interface Connects coating or film to the reinforcement. Construction and adhesion, including the failure mode after relevant conditioning.
Surface finish Changes exposed-surface performance such as dirt pickup and cleanability. Acrylic/PVDF grade, treated face, maintenance and welding requirements.

Knife coating and lamination describe a route

Knife coating meters a PVC coating compound onto the textile before thermal processing forms the coating. Lamination joins a preformed film to the reinforcement. Bonding may use heat and pressure or an adhesive system. Ask which route is actually offered: the word laminated does not prove that a separate glue layer is present.

Neither route alone supplies a tensile value, a tear value or a service-life promise. Compare the finished constructions and the conditions in which they will work.

02

Knife-coated vs laminated: performance and lifespan

Two materials can have the same gsm and still use different yarns, PVC formulations and bonding structures. The table below compares the questions each route raises; it is not a league table of untested product values. Begin with a similar reinforcement, mass, intended use and exposure, then compare matched reports.

Physical performance

Property Knife-coated PVC Laminated PVC Fair comparison
Tensile strength Depends on reinforcement, direction and finished construction. Also depends on reinforcement, direction and finished construction. Same tensile method, specimen width and conditioning; report warp/weft and elongation.
Tear resistance Yarn, weave and the coating’s effect on yarn movement matter. Yarn, weave and film/bonding construction matter. Same tear method and direction. High tensile strength does not establish high tear resistance.
Adhesion / peel Evaluate coating-to-textile attachment and retained adhesion after relevant ageing. Evaluate film-to-textile attachment; assess any adhesive layer where present. Same method, units and direction; identify which interface or material failed.
Flexing and cold bending PVC formulation, plasticisation, thickness and structure govern the response. Film formulation, bonding structure and thickness govern the response. Distinguish repeated flexing, cold bending and static cold exposure. Match conditions and endpoints.
Abrasion / surface retention Outer-layer formulation, thickness, finish and contact conditions matter. Film formulation, finish and contact conditions matter. Same abrasive system, load, cycles and failure criterion; inspect the relevant function after wear.
Appearance / gauge Coating amount and texture can be adjusted; uniformity depends on production control. Preformed film can support controlled appearance and film gauge; finished uniformity still needs checking. Compare finished thickness, mass and tolerances. Smoothness is not proof of longer life.

Water, fabrication and long-term use

Property Knife-coated PVC Laminated PVC What to verify
Water barrier / edge wicking An intact PVC layer can resist water; exposed reinforcement and seams remain separate routes. An intact film can also resist water; exposed edges and seams still need assessment. Through-surface water penetration, edge wicking and seam leakage are three separate checks.
Welding Weldable constructions are possible; finish and process must be qualified. Weldable constructions are also possible; lamination does not inherently prevent welding. Trial-weld the offered material with the proposed preparation and equipment. Assess the completed seam.
Lightfastness / weathering Pigments, stabilisers, finish, colour and exposure affect results. The same variables affect results. Identify the product, method, scale and endpoint. No universal process-based lightfastness grade applies.
Long-term durability Watch coating wear, formulation ageing, finish retention, adhesion and seams. Watch the same properties plus long-term film-to-textile attachment and any adhesive layer. Compare relevant aged properties, exposure history and maintenance assumptions.
Whole-fabric service life A process name does not establish a fixed number of years. A process name does not establish a fixed number of years. Request a grade-specific expectation and its evidence, conditions, limitations and separate warranty terms.

Practical conclusion: choose the construction that meets the application and has matching evidence. Do not assign all knife-coated fabrics a longer life, all laminates a lower strength, or either route a fixed lifespan multiplier.

03

What acrylic and PVDF surface finishes do

A surface finish is a thin working layer over the PVC, where specified. Suitable formulations can reduce dirt pickup, improve cleanability and slow plasticizer migration. A PVDF finish on PVC is still a finished PVC composite; it is not a PTFE-coated glass fabric or a sheet of solid PVDF.

Separate the function from the label

Function What it can mean Useful evidence
Dirt resistance / easy cleaning Less dirt retention or easier removal under defined conditions. Named soil, cleaning procedure, comparison and appearance after cleaning.
Migration barrier A suitable finish can reduce movement of plasticizer toward the surface. Grade-specific assessment and compatibility with storage, printing, adhesives and cleaning.
Surface appearance Gloss, matt appearance or texture can be specified. Approved appearance sample, colour reference and agreement on variation.
Weather-exposed surface The finish forms part of the material’s exposure response. Relevant weathering, appearance and property-retention evidence for the offered material.

Plasticizers help flexible PVC remain flexible. Their movement is one ageing mechanism among several. A finish is not a permanent seal against every ageing process, chemical or contaminant.

Repeated rubbing, folding and unsuitable cleaning can wear or damage the finish. Thickness alone does not describe coverage, adhesion or effectiveness. A micrometre figure should identify dry or wet film, the treated face or faces, the measurement method and tolerance. It is separate from total fabric thickness.

04

Finish function, fabric lifespan and warranty

Before comparing years, ask what the years describe. Surface appearance, ease of cleaning, a functional topcoat, the fabric’s useful service and a contractual warranty are different subjects.

Surface treatment Factory-supplied functional reference How to use it
Acrylic finish About 2years Reference for surface-treatment function only, subject to the applicable grade, exposure, handling and maintenance.
PVDF finish About 5years Reference for surface-treatment function only; not a universal period for every PVDF formulation or environment.

These are Duletai’s factory-supplied reference periods for the surface treatments discussed here. They are not whole-fabric service-life figures or unconditional warranties. For an order, agree the applicable grade, which function is being assessed, acceptable change and the conditions attached to the expectation.

A finish does not suddenly stop working on an anniversary, and a fabric does not automatically become unusable when one surface function changes. Equally, an intact-looking surface cannot prove that every seam or mechanical property remains adequate.

Keep the three statements separate

  • Functional reference period: what a defined finish is expected to do under stated conditions.
  • Expected fabric service life: a grade- and application-specific assessment of the whole material.
  • Warranty: the written contractual coverage, exclusions and remedies.
05

PVDF and welding: qualify the actual grade

“PVDF” is not a complete welding instruction. Formulation, finish coverage, the faces being joined, equipment and preparation all affect fabrication. Some systems are designed for welding as supplied; others require specified treatment of the overlap. Do not transfer instructions from one formulation to another.

Duletai describes a newer PVDF finish formulation as weldable. Evaluate the specific offered grade and its procedure. Terms such as “pure PVDF” need a written definition of the formulation claim; the phrase alone does not establish resin content, eliminate preparation or guarantee a seam result.

Before production welding

  1. Identify the product grade, batch, finish and treated faces.
  2. Obtain the recommended welding route and any overlap preparation.
  3. Trial-weld actual production material using the intended equipment.
  4. Record the process settings and inspect the completed seam and failure mode.
  5. Where exposure warrants it, assess seam performance after relevant conditioning or ageing.

A strong coating-to-textile adhesion result is useful, but it is not a substitute for testing the fabricated weld. Conversely, a locally strong weld does not establish the durability of every coating interface.

06

Waterproofing, anti-wicking and mildew are separate

Water can follow more than one route. Resistance through an intact coated face is different from leakage at a seam, hole or fitting. At an exposed cut edge, water can contact the reinforcement and move through small spaces between filaments and yarns by capillary action.

Water at an exposed cut edge can move along the reinforcement, a different route from through-surface penetrationFOLLOW THE WATER ROUTEIntact surfaceNo through-surface path shownExposed edgePossible movement through yarn / filament gapsWater-path schematic; not a measured rise or a product test.
The internal water path begins at exposed reinforcement in this schematic. It does not show water passing through an intact PVC face.

Anti-wicking treatment aims to limit that movement through the reinforcement. It does not replace the PVC barrier, a suitable seam or a protected edge. A surface water-beading demonstration also does not, by itself, establish low edge wicking.

Question Relevant property What it does not establish
Does water penetrate the intact face? Resistance to through-surface water penetration under stated pressure/time. Edge wicking or completed-seam watertightness.
Does water rise along exposed reinforcement? Anti-wicking performance under a specified liquid-rise or agreed edge-exposure method. An anti-mildew result or the lifespan of the whole material.
Does the material resist specified fungal growth or attack? A suitable biological test for the material and intended use. Low wicking, permanent stain prevention or leak-free fabrication.

Persistent moisture and contamination can create conditions for staining or biological growth. Wicking, dirt, microbes and loss of adhesion should nevertheless be investigated separately. Water reaching reinforcement does not prove that mould or delamination must follow, or identify the sole cause of an observed defect.

07

Duletai’s dip-and-pad treatment sequence

Duletai describes treating the woven base fabric with an anti-wicking emulsion through a dip-and-pad process, followed by drying. The pad-treatment step is completed 24h before the subsequent production stage.

Duletai describes dip-and-pad treatment, drying and subsequent production; pad treatment is completed 24hours in advanceCOMPLETED IN ADVANCEDip + padwoven reinforcementDryingSubsequentproduction stagePad treatment completed 24h before later productionNot 24h of continuous immersion; no curing duration is specified here.
Company-described sequence. The 24h reference is advance completion of pad treatment, not a specified immersion, drying or curing duration.

This is not a claim that the fabric remains immersed for 24h. It also does not specify a24h cure, drying temperature or chemical reaction time. Those process conditions belong to the actual production specification.

Yarn-stage and fabric-stage routes

Anti-wicking measures may be introduced at different stages. Buyers should ask how the chosen treatment is controlled and whether its effect is retained through later processing. The finished material, including exposed edges and fabricated details, is the relevant comparison.

The treatment should not be imagined as filling solid polyester filaments with liquid. Nor does the stage of application prove that one route is universally more effective. A process explanation and a matched finished-material result should support each other.

08

Read test reports without mixing the measurements

Record the exact method and edition, specimen construction, direction, conditioning and result units before comparing two reports. An ISO number identifies a method; it does not automatically specify a universal pass value or prove that a Duletai product was tested.

Measurement Example method / scope Check before comparing
Tensile / elongation ISO 1421:2016 — tensile strength and elongation; different specimen methods. Method, specimen width, warp/weft, conditioning and elongation.
Tear ISO 4674-1:2016 — constant-rate tongue or trouser tear. Specific tear method, direction and how the force is reported.
Coating adhesion ISO 2411:2024 — adhesion strength of coated fabrics. Interface, direction, units, failure mode and any aged results.
Repeated flexing ISO 7854:1995 — damage from repeated flexing using distinct methods. Chosen method, cycles, conditioning and damage endpoint.
Cold bending ISO 4675:2017 — bending after defined low-temperature exposure. Temperature, exposure and assessed damage; do not equate this with all field cold behaviour.
Abrasion ISO 5470-1:2016 — Taber abrasion of coated fabrics. Abrasive system, load, cycles, mass loss or agreed endpoint.
Water penetration ISO 1420:2016 — hydrostatic pressure and time applied to coated fabric. Pressure/time and method. This is not an exposed-edge wicking measurement.
Lightfastness ISO 105-B02 — artificial-light colour-fastness assessment. Applicable method, colour, reference scale and result. Lightfastness is not overall weathering or service life.
Edge wicking An agreed, fully described liquid-rise or edge-exposure method. Liquid, direction, edge preparation, depth, time, reference point and number of specimens.

What a liquid-rise comparison needs

Use the same liquid, sample preparation, direction, immersion depth, environment, duration and distance origin. Identify whether the stated result is the maximum, mean or another measure. Ink composition can change the test behaviour; an ink result should not silently become a pure-water result.

A lower rise in a matched test is useful evidence for that measurement. It cannot be converted directly into an equal-percentage improvement in strength, total performance or fabric lifespan.

Read colour grades correctly

Blue-wool references and grey-scale assessments are different reporting tools. A colour-fastness grade also needs its method and colour identified. Fading resistance does not prove coating adhesion, retained tensile strength or a guaranteed number of outdoor years.

09

Assess durability under the actual exposure

Outdoor service combines sunlight, temperature, moisture, pollutants and mechanical handling. Hotter, drier conditions do not automatically extend life: a change that reduces one moisture-related exposure may increase heat or UV stress. Climate descriptions alone are not a durability assessment.

For repeated-use covers, folding and contact abrasion may be decisive. For a long-term roof or enclosure, persistent moisture at details, surface condition, seam integrity and retained mechanical properties may deserve more attention. Evaluate the actual assembly rather than assigning a generic “good climate”.

Useful evidence for a service-life discussion

  • The exact grade and construction used in the evidence.
  • Exposure location, orientation and material temperature where relevant.
  • Initial and aged appearance, adhesion, mechanical and seam properties.
  • The definition of acceptable performance and its failure criterion.
  • Cleaning, handling, inspection and repair assumptions.

Accelerated exposure hours cannot be multiplied by a universal factor to obtain outdoor years. A predictive claim needs correlation relevant to the material, environment and failure mode.

Melting snow can prolong wet contact around vulnerable details, but snow loading and structural adequacy are separate engineering questions. Anti-wicking treatment does not replace structural design, drainage, inspection or snow-load management.

10

Choose the specification for the application

Use / exposure Priorities to discuss Evidence or detail to request
Long-term tents and enclosures Finish specification, weathering, adhesion, mechanical retention and seams. Grade-specific exposure evidence, fabrication procedure and inspection plan.
Covers repeatedly folded or handled Flexibility, low-temperature bending where relevant, abrasion and edge wear. Relevant flex/cold/abrasion results and practical handling restrictions.
Dusty or dirty locations Dirt retention, cleanability and compatibility with expected contaminants. Approved cleaning method and appearance after representative cleaning.
Details exposed to prolonged moisture Barrier continuity, edge wicking, seam quality and drainage. Separate water-penetration, edge-exposure and completed-detail assessments.
Printed or bonded surfaces Compatibility of finish, ink, adhesive and intended exposure. An approved compatibility trial on the offered grade; low dirt pickup does not prove print adhesion.

A coating route is one part of the specification. It should be discussed together with reinforcement, formulation, surface treatment, anti-wicking requirements and fabrication. Regulatory or fire-performance needs also require their own applicable reports.

11

Cleaning, inspection and troubleshooting

Use the material supplier’s approved cleaning procedure. Remove loose contamination gently, use compatible products and tools, and follow the specified rinsing and drying instructions. Avoid assuming that a stronger solvent, harsher abrasive or higher cleaning pressure is acceptable. Check compatibility on a small area when the procedure calls for it.

Store and handle material as specified; persistent dampness and trapped contamination deserve attention. Inspect high-contact zones, fold lines, exposed edges, fittings and seams. Address drainage and local rubbing rather than relying on a finish to overcome a poor detail.

Observed symptom Possible issues to investigate Useful first checks
Dark marks near a cut edge Liquid movement, retained dirt or biological growth; appearance alone cannot identify which. Location, exposure, edge construction, cleaning history and representative samples.
Film or coating lifts from reinforcement Interface weakness, processing or ageing may be involved. Batch identification, failure interface and matched initial/conditioned adhesion tests.
Sticky or dirty surface Contamination, compatibility or migration-related change may contribute. Cleaning and storage records, contacting materials and surface examination.
Seam leaks or separates Preparation, compatibility, weld process or detail design may be relevant. Actual seam sample, process record and agreed seam/watertightness assessment.
Cracking at folds Formulation, temperature, repeated flexing and local wear may contribute. Handling conditions, material grade and relevant bend/flex results.

Do not diagnose every dark edge as mildew or every separation as proof of one manufacturing route being inferior. Keep an unused reference sample where possible and compare the actual failed detail with it.

12

A practical order and acceptance checklist

Give Duletai the intended use, exposure, fabrication route and most important failure risk. Then agree a written specification for the exact offered material.

  • Construction: polyester filament reinforcement, yarn/weave, coating or lamination route and any bonding layer.
  • Finished properties: mass, thickness, tolerances and required directional physical results.
  • Surface: finish grade, treated faces, function, maintenance and compatibility.
  • Water routes: through-surface resistance, anti-wicking and seam/detail requirements separately.
  • Fabrication: approved joining method, preparation, trial samples and acceptance criteria.
  • Evidence: matching product/batch, method, edition, specimen conditions, initial/aged results and failure mode.
  • Years and warranty: define any finish-function reference, expected fabric service and contractual warranty separately.

That makes two offers easier to compare and gives incoming inspection a clear target. A label such as “PVDF”, “anti-wicking” or “knife-coated” should begin the technical discussion, not end it.

FAQ

Is knife-coated tarpaulin always stronger than laminated tarpaulin?

No universal ranking follows from the process name. Reinforcement, formulation, bonding and finished structure matter. Compare matched tensile, tear, adhesion and relevant aged results for the offered grades.

Does PVDF mean the complete fabric will last 5years?

No. The reference of about 5years discussed here is a Duletai factory reference for surface-treatment function. Whole-fabric service life and a written warranty are separate and depend on the specified product and conditions.

Can all PVDF-finished fabrics be welded without preparation?

No. Use the procedure for the actual grade and validate a trial seam. A newer weldable formulation should be assessed on its own specification; instructions from a different PVDF system should not be assumed to apply.

Does anti-wicking replace waterproof seams or anti-mildew treatment?

No. It targets moisture movement through the reinforcement. Barrier continuity, seam watertightness and resistance to specified biological exposure require their own assessment.

Is Duletai’s base fabric immersed for 24h?

No. Duletai describes dip-and-pad treatment followed by drying, with the pad-treatment step completed 24h before subsequent production. That does not define 24h of immersion, drying or curing.

Can a liquid-rise result be converted into a fabric lifespan?

Not directly. A matched liquid-rise test measures movement under its stated conditions. A service-life prediction needs separate evidence relevant to the material, exposure and failure criteria.

Does a higher lightfastness grade prove better overall durability?

It describes colour change under a specified method, not every mechanical or chemical property. Check the method, scale and colour, then assess weathering, adhesion and mechanical retention separately.

What should I send when asking for a quotation?

Send the application, exposure location, panel dimensions, handling and joining method, required finish and water-related functions, and the reports or acceptance criteria your project needs.

SPECIFY THE MATERIAL WITH DULETAI

Tell us the intended application, exposure and fabrication method, and the properties that matter most. We can discuss the offered construction and the information needed for a meaningful comparison.

Discuss your fabric requirements · Read a PVC tarpaulin datasheet · Understand fire-performance standards

REFERENCES

The following method summaries and technical education explain what measurements mean. They do not establish test results or certification for a Duletai grade. Scope information checked on 17 October 2026; agree the required edition and complete procedure with the laboratory.

  • ISO 1421:2016 — tensile and elongation
  • ISO 4674-1:2016 — tear methods
  • ISO 2411:2024 — coating adhesion
  • ISO 7854:1995 — repeated flexing
  • ISO 4675:2017 — low-temperature bending
  • ISO 5470-1:2016 — Taber abrasion
  • ISO 1420:2016 — water penetration
  • Q-Lab — lightfastness and weathering
  • Q-Lab — exposure and service-life correlation
PVC Tarpaulin Datasheets Explained

  • 0
admin
Thursday, 15 October 2026 / Published in Technology

Views: 156

DULETAI MATERIAL GUIDES · UNDERSTAND THE SHEET

A fabric datasheet can look like a wall of numbers. What does 1000D actually describe? Why are thickness, weight, tensile strength and tear strength separate rows? And which details are options rather than features included in every roll?

Let’s read one sheet from top to bottom. We use the 15 rows on Duletai’s DuraTarps DLT-5210 product page as a real example, then explain the terms in plain English. The listed figures are the website’s example values; where the sheet leaves out a unit or test condition, we keep that distinction visible.

WATCH THE VIDEO

Watch our six-minute guide to reading a PVC tarpaulin datasheet, from polyester filament yarns and fabric weight to strength, finishes and ordering details.

BUYER TAKEAWAY

Read a value together with its unit, direction and test conditions. A bigger number answers only the question that particular measurement asks.

ANNOTATED TECHNICAL DATASHEET

Use this sheet as a reading template. The middle column reproduces the DLT-5210 example values; the right column explains how to read them. Select a numbered field for its detailed explanation below.

DuraTarps DLT-5210 | Ultra Wide Tent Fabric
Parameter Example value Reading note
01Base fabric: 1000D*1000D 30*30 Polyester filament yarns. D is yarn linear density; confirm the counting unit for 30×30.
02Thickness: 0.58mm Finished coated-material thickness; check the measurement pressure and tolerance.
03Weight: 750gsm Mass per unit area. A higher gsm is not a strength rating.
04Width: 5.0m Roll width; confirm usable width and edge allowances.
05Roll length: 50m Length along the roll. Multiply width by length to calculate area.
06Tensile Strength: 3300N/5cm Force in tension; check the test method and warp/weft results.
07Tearing strength: 430N/5cm Resistance to tear growth; verify the test method and reported unit.
08Peeling strength: 100N/5cm Layer adhesion; clarify which interface was tested.
09Surface: Glossy/Matte Surface appearance; select the required finish.
10Options: Blackout,Arcylic/PVDF coating, Flame retardant, Anti-cold/mildew/UV Specify the required treatments. Chapter 10 also explains mildew, antibacterial, low-wick and other functional options.
11Colour: Customized Agree a colour reference and acceptable variation.
12Temperature: -20~+70(°C) Clarify use or storage conditions and exposure duration.
13FR certification: Customized B1, B2, M1, M2, NFPA701, DIN75200; Choose the required test and request the matching material report.
14Packing: Paper tube+PE film+Craft paper Core and protective wrapping; confirm the package details.
15MOQ: 3000yards for customization/ 100yards for in-stock Custom and stock order quantities; confirm current terms and the yard basis.

Example values are from the linked DLT-5210 product sheet. Notes explain the entries and the details to check for a specified order; they do not add test results.

READ ONE FIELD AT A TIME

Choose a field to open its explanation. Scroll inside long chapters; click the chapter heading again to close it.

01

BASE FABRIC

Example sheet · source wording1000D*1000D 30*30

What this row means

Base fabric is the woven reinforcement inside the coated material. Duletai uses polyester filament yarns for its base fabrics, including the DLT-5210 example discussed here. Think of the yarn network as a supporting skeleton and the PVC layers as part of the finished composite. The base-fabric description does not describe the finished material on its own.

Read the unit or notation

D means denier: a yarn linear-density unit. A 1000D yarn has a mass of 1000g per 9000m of yarn. It is neither a diameter nor a force rating. The two 1000D figures normally refer to yarns in the two fabric directions; confirm the supplier’s order of notation.

How it is measured or checked

Thread count is a separate measurement: how many yarns cross a stated counting length in each direction. Weave is another separate choice: the way those yarns cross over and under one another. Counting yarns, describing their linear density and measuring finished-fabric strength answer three different questions.

Why it matters in use

The reinforcement matters when a cover is tensioned, cut, folded or joined. Two materials described as 1000D can still behave differently because their fibres, yarn quality, weave, thread count, coating and processing differ.

Before comparing two sheets

The example sheet does not give the unit for 30*30, specify the weave, or state the direction order. Do not silently read it as 30 threads/inch or call this model Panama. Compare finished tensile and tear results under matching methods, as well as the base-fabric construction.

Plain: one over, one under

Plain over-one-under-one weaveBlue: warpOrange: weft

One generic interlacing pattern.

Basket: pairs work together

Generic two-by-two basket weaveBlue: warpOrange: weft

Generic 2×2 grouping, not a model identification.

Warp and weft: which way is which?

Warp yarns usually follow the length of a woven roll, along its selvedges; weft, also called fill, crosses the width. Keep the supplier’s direction markings when cutting samples or panels. If a report has two strength values, identify the direction beside each value instead of treating them as interchangeable.

Why the counting unit changes the answer

For a hypothetical construction, 30 threads/inch is about 11.81 threads/cm. A different hypothetical count of 30 threads/10cm is 3 threads/cm. Both can appear as the number 30 if the denominator is missing. These examples explain the notation; neither establishes DLT-5210’s density unit.

Plain weave and basket weave

Plain weave alternates over one yarn and under the next. In a 2×2 basket weave, pairs work together, crossing over and under other pairs. Panama is commonly used for basket constructions, but the actual grouping must be specified. The diagrams show generic weave concepts, not a verified construction for this example model.

What 1000D does not tell you

Duletai’s yarns are polyester filament yarns. The 1000D value alone does not specify the number of filaments per yarn, yarn strength, thread count or the total gsm of the coated fabric. Ask for those construction details separately if they matter to the application.

Read more: CottonWorks: yarn numbering · CottonWorks: basic woven designs

02

THICKNESS

Example sheet · source wording0.58mm

What this row means

Thickness is the distance between the two faces of the finished sheet. Millimetres are a length unit; this row is not a measure of mass or strength.

Read the unit or notation

0.58mm is the website’s listed thickness. The table does not state a tolerance or whether the number is a typical, minimum, nominal or other specified value.

How it is measured or checked

A thickness gauge measures the distance under a stated contact pressure. ISO 2286-3 describes a method for coated fabrics at a specified pressure. Soft or textured surfaces can give different impressions by touch, so a hand-feel comparison is not a measurement.

Why it matters in use

Thickness affects clearances, folded bulk and how a converter approaches cutting or joining. It does not by itself prove better cold performance, abrasion resistance or water resistance.

Before comparing two sheets

Match the measurement method, pressure, sampling positions and tolerance. Two equally thick constructions may contain different amounts of coating and reinforcement.

Read more: ISO 2286-3: thickness at specified pressure

03

WEIGHT

Example sheet · source wording750gsm

What this row means

Here, weight means mass per unit area. A 1m×1m piece at the listed 750gsm would have a nominal material mass of 750g, not including separate packaging or fittings.

Read the unit or notation

gsm means g/m²: grams per square metre. An alternative area-mass unit is oz/yd². Using the NIST conversion factor, 750gsm is approximately 22.12oz/yd²; that is a calculated equivalent, not an additional value from the original table.

How it is measured or checked

Area mass is determined from the mass of a known sample area under the specified procedure. ISO 2286-2 distinguishes total area mass from the area mass of the coating and the substrate.

Why it matters in use

Area mass helps estimate material handling and compare construction when the other details match. It cannot tell you how much is reinforcement and how much is coating unless that split is provided.

Before comparing two sheets

Check the unit, conditioning, sampling and tolerance. Added coating can increase gsm without a proportional increase in tensile or tear strength. Read the strength rows separately.

Read more: ISO 2286-2: mass per unit area · NIST: unit-conversion factors

04

WIDTH

Example sheet · source wording5.0m

What this row means

Width is the dimension across an unrolled sheet, from one side toward the other. It is different from the length along the roll.

Read the unit or notation

The website lists 5.0m. The table does not distinguish nominal width from usable finished width or give an edge allowance.

How it is measured or checked

Width is measured across the roll under an agreed roll-measurement procedure; ISO 2286-1 covers methods for roll length, width and net mass. State what edges are included when specifying usable width.

Why it matters in use

A wider roll may allow a larger panel with fewer joins, but the result depends on the actual cut layout, overlaps and edge finishing. Width alone does not establish a percentage saving.

Before comparing two sheets

Check usable width, width tolerance, selvedge treatment and cutting direction. Allow for seam overlap and any parts of the edge that cannot be used in the finished product.

Read more: ISO 2286-1: roll length, width and net mass

05

ROLL LENGTH

Example sheet · source wording50m

What this row means

Roll length runs in the unrolling direction. Together, length and usable width determine the available area before cutting and joining allowances.

Read the unit or notation

The listed length is 50m. Metres describe a length, while m² describes an area. They should not be substituted for each other in a quote or order.

How it is measured or checked

Measure roll length under the agreed procedure and record its tolerance. ISO 2286-1 addresses roll length, width and net mass; it is an example of a measurement framework, not evidence that this listed roll was tested to it.

Why it matters in use

Worked example: if width is exactly 5m and length exactly 50m, the rectangular area is 250m². If that whole area is also exactly 750gsm, the calculated material mass is 187.5kg. This arithmetic does not establish the shipped roll’s actual net or gross mass.

Before comparing two sheets

Use measured or agreed usable dimensions and area mass when needed. Account separately for core, wrapping, fittings, trimming and manufacturing tolerances.

An unrolled rectangle separates width from roll length; area equals width times length. Width 5mRoll length 50m250m²Worked rectangular-area example
Hypothetical exact dimensions for arithmetic. Cutting allowance, overlap and actual roll dimensions are separate.

Read more: ISO 2286-1: roll length, width and net mass

06

TENSILE STRENGTH

Example sheet · source wording3300N/5cm

What this row means

Tensile testing asks how much pulling force an initially intact specimen resists as its ends are drawn apart. It answers a different question from the force needed to extend an existing tear.

Read the unit or notation

N is the newton, a unit of force. In an N/5cm expression, the width basis must be read with the actual test method. Do not read 3300N/5cm as a safe hanging load for a cover, attachment or tent.

How it is measured or checked

ISO 1421 describes a strip method for tensile strength and elongation at break, and a grab method for tensile strength. Specimen preparation and grip arrangement matter, so results from different methods are not automatically interchangeable.

Why it matters in use

The result helps discuss how the material behaves under pulling. A complete product also depends on shape, seams, reinforcement, fixing points and loads; the material number is not a structural design value.

Before comparing two sheets

The example gives one value without method, direction, conditioning or a typical/minimum designation. Ask for the method and separate warp/weft results before ranking another material against it.

Pull an intact specimen

tensile principle schematic, not a specified laboratory specimen

Tensile principle.

Extend a tear

tear principle schematic, not a specified laboratory specimen

Tear principle; geometry depends on method.

Separate layers

peel principle schematic, not a specified laboratory specimen

Confirm which interface is tested.

Read more: ISO 1421: tensile methods

07

TEARING STRENGTH

Example sheet · source wording430N/5cm

What this row means

Tearing concerns the force needed to start or continue a tear in a specified specimen. In a simple explanation, imagine a cut or damaged edge being pulled further open, rather than an intact strip being pulled straight apart.

Read the unit or notation

The original table says 430N/5cm. We retain that exact expression. The table does not explain its width basis or method, so we do not silently change it to 430N or assume it matches another tear result.

How it is measured or checked

ISO 4674-1 uses different specimen arrangements: method A is tongue tear and method B is trouser tear. Other tear methods use other geometries. Their results answer method-specific questions rather than providing a universal conversion.

Why it matters in use

This property matters when discussing damage near an edge, opening or attachment. It should be considered alongside reinforcement and product construction, not treated as a guarantee that a puncture can never spread.

Before comparing two sheets

Confirm the reported unit, test method, specimen direction and result basis. A higher tensile number does not automatically mean better tear performance.

Read more: ISO 4674-1: tear methods

08

PEELING STRENGTH

Example sheet · source wording100N/5cm

What this row means

Peeling describes the resistance to separating joined layers. The first question is which layers: coating from its substrate, a layer within a laminate, or two pieces joined in a welded seam?

Read the unit or notation

The table lists 100N/5cm, but does not identify the interface or method. A force stated on the same width basis can still describe different tests.

How it is measured or checked

ISO 2411 addresses coating adhesion strength of coated fabrics. A welded-seam peel test can address a different joint. Also record the failure mode: an interface separating, a coating tearing within itself, or the fabric breaking are different observations.

Why it matters in use

The distinction matters when investigating delamination, folding damage or a seam problem. Strong original material and a well-made joint are separate questions.

Before comparing two sheets

Confirm the layers being separated, method, width, direction, dry/wet or aged condition, and how the force result is summarised. Do not relabel the listed number as verified weld strength.

Read more: ISO 2411: coating adhesion

09

SURFACE

Example sheet · source wordingGlossy/Matte

What this row means

Glossy and matte describe surface appearance. Glossy surfaces show more distinct specular reflections; matte surfaces give a less sharply reflected appearance under the same viewing conditions.

Read the unit or notation

These are descriptive options in this table, not a numerical gloss reading. The slash does not specify whether both faces are identical or which version a particular order includes.

How it is measured or checked

Compare finish using the same light, viewing angle and sample conditions. A measured gloss comparison would also need an agreed method and measurement geometry.

Why it matters in use

Finish influences the intended visual appearance and should be agreed alongside any printing or conversion requirements. It does not on its own establish strength, slip resistance or outdoor lifetime.

Before comparing two sheets

Confirm which face and finish are being offered and approve a representative sample. A glossy sample and a matte sample photographed under different lighting are not a controlled comparison.

10

OPTIONS

Example sheet · source wordingBlackout,Arcylic/PVDF coating, Flame retardant, Anti-cold/mildew/UV

What this row means

An options row lists possible requirements to discuss. It does not mean every roll automatically includes every item, or that combining them leaves all other properties unchanged.

Mildew versus bacteria · Additional functional options

Read the unit or notation

These words are feature categories, not measured results. Each needs its own acceptance criterion. The source spells acrylic as Arcylic; the explanation uses the standard spelling without changing the copied source value.

How it is measured or checked

Define each option through a property, a test or comparison method where applicable, and the condition after which the result is required. No single test verifies every functional option.

Why it matters in use

Choose the options relevant to the actual project, then agree the finished construction and conversion requirements. Do not use one option name to infer another property, such as treating blackout as a thermal-insulation rating.

Before comparing two sheets

Check whether an item is standard or optional for the offered version, what combination is available, and which written requirement and supporting result apply to the supplied material.

Blackout

Reduced light transmission is the subject. Agree a transmission or opacity requirement and how it is measured; the word alone does not establish zero transmission, heat insulation or a particular internal layer.

Acrylic / PVDF coating

These name possible surface-treatment chemistries. They are not interchangeable names for the same finish. Confirm which treatment, which face, its intended purpose and compatibility with printing or welding; no thickness, recipe or service life is stated here.

Flame retardant

Specify the required standard, classification or pass result and the tested construction. The option is not a universal fireproof claim, nor evidence that every grade named elsewhere applies to every version.

Anti-cold

Ask about the required low-temperature behaviour and test, especially if the material will be folded or flexed while cold. A temperature number without the action and conditions leaves the practical question unanswered.

Anti-mildew / Anti-fungal

This concerns resistance to fungal growth on the material, particularly in humid service or damp storage. Agree the organisms, exposure conditions, growth assessment and required result. Clean handling and dry storage remain part of cover care.

Anti-UV

Ask which property is assessed after an agreed UV/weathering exposure: colour, appearance, cracking or retained strength, for example. Exposure conditions and the endpoint matter; no outdoor lifetime follows from the label alone.

Anti-mildew, antibacterial and antimicrobial

Anti-mildew and anti-fungal treatments address fungal growth. Antibacterial treatments address bacteria. Antimicrobial is a broader description: the claimed organisms and measured effect still need to be identified. These terms should not be treated as interchangeable test results.

For example, a humid tent fabric may need fungal-growth resistance, while a frequently cleaned coated textile may have a separate antibacterial requirement. Low-wick treatment addresses water movement through the reinforcement, so it is another specification item rather than a synonym for either treatment.

Additional functional options

PVC-coated fabric specifications can include more than the six labels in the example row. The options below explain other functions you may encounter. Availability and compatible combinations depend on the selected grade.

Option Purpose and typical use What to specify
Antibacterial / antimicrobial Aims to control specified microorganisms. Useful for coated textiles selected for hygiene-sensitive or frequently cleaned uses. Identify the organisms, suitable method, contact time and result after the agreed cleaning or ageing treatment.
Low-wick / anti-wicking Limits capillary water migration along exposed base-fabric yarns, especially at cut edges and fabrication details. Request an agreed cut-edge wicking assessment and suitable edge sealing; a waterproof coating alone does not establish low-wick performance.
Antistatic / static-dissipative Controls electrical behaviour where static build-up matters, such as selected industrial curtains, doors or ducting. State the electrical property, target range, method and conditioning. Check the finished installation requirements for the intended use.
Easy-clean / soil- or stain-resistant finish A selected topcoat can make dirt removal and routine maintenance easier on exposed covers or membranes. Agree the staining or soil, cleaning products, number of cleaning cycles, and acceptable appearance; check welding and printing compatibility.
Chemical, oil or acid/alkali resistance Specially selected grades address contact with named liquids or cleaners in a defined application. Give the exact chemical, concentration, contact time and temperature. Assess the coating, seams and retained properties together.
Print-compatible surface A finish selected for logos, graphics or printed covers must suit the ink and printing process. Approve an actual print trial for ink adhesion, curing, rubbing and weathering performance; confirm the required coated face.
Hydrolysis-resistant grade A specialist requirement for prolonged moisture or liquid exposure, including some containment materials. Agree the exposure medium, temperature, duration and retained properties. Confirm compatibility with the complete material construction.

Choose a test suited to the coated textile

ISO 20743 covers antibacterial textile products and offers different inoculation approaches. The laboratory should select a suitable approach for the intended use and surface. ISO 22196 explicitly excludes antibacterial-treated textile products, even when coated or laminated, and refers to ISO 20743; a PVC surface does not automatically make a textile a plastics test specimen.

For a fungal or antibacterial claim, ask which organisms were tested, what endpoint was measured and whether the result applies after the intended cleaning or ageing. A material-treatment result does not replace cleaning or establish a medical or infection-prevention claim.

11

COLOUR

Example sheet · source wordingCustomized

What this row means

Customized means colour is a requirement to agree for the offered material. It is not a colour code, a stock list, or a promise of an exact match under every light.

Read the unit or notation

No colour reference, tolerance or colour-difference limit is stated. Use an agreed physical reference or a specified colour system rather than a screen image alone.

How it is measured or checked

Observe comparison samples under agreed lighting and viewing conditions. If instrumental colour measurement is required, agree the method and limits instead of inventing a numerical tolerance.

Why it matters in use

Colour approval helps manage the appearance of adjacent panels, replacement parts and repeat orders. Surface texture and gloss can change the perceived match.

Before comparing two sheets

Confirm the reference, approved finish, matching conditions and whether the order involves multiple production batches. Check current availability rather than assuming every custom colour is stocked.

12

TEMPERATURE

Example sheet · source wording-20~+70(°C)

What this row means

This row gives a temperature range but does not define the activity or test to which it applies. Storage, stationary use and repeated folding are different conditions.

Read the unit or notation

°C means degrees Celsius. The source’s -20~+70(°C) is retained as listed. The table gives no duration, flexing procedure, load or acceptance criterion.

How it is measured or checked

A low-temperature bend or cracking test observes behaviour after a specified preparation and action. A stated operating range is not automatically the result of that test, and is not a welding-machine setting.

Why it matters in use

For a cover that will be rolled or packed in cold weather, ask specifically about cold flexing. For hot conditions, state the exposure, duration and contact conditions rather than relying on the range alone.

Before comparing two sheets

Confirm whether the numbers describe operating, storage or test conditions, and what change or failure is being assessed. Do not interpret +70°C as a general processing temperature.

13

FR CERTIFICATION

Example sheet · source wordingCustomized B1, B2, M1, M2, NFPA701, DIN75200;

What this row means

The source uses the heading FR certification, but its value mixes grade labels and standard names, preceded by Customized. Read it as a list of fire-related requirements to clarify for an offered version.

Read the unit or notation

These are not units of force, mass or temperature. They cannot be arranged into a single universal league table, and a label without its standard and version can be ambiguous.

How it is measured or checked

Fire tests expose specified specimens under defined conditions and report the result required by that method or classification route. A grade label, a pass result and a standard number are different kinds of information.

Why it matters in use

Start with the requirement for the actual application and destination. For an explanation of the main standard families, use Duletai’s fire-standards guide rather than assuming that one label covers every installation.

Before comparing two sheets

This row does not prove that DLT-5210 has simultaneously passed every listed requirement. Confirm the full designation, applicable offered construction and supporting report. Do not use a generically named attachment as model-specific certification.

Read more: Duletai: PVC Tarpaulin Fire Standards

14

PACKING

Example sheet · source wordingPaper tube+PE film+Craft paper

What this row means

Packing describes how the roll is prepared for delivery. The paper tube is the core, and the film and paper describe wrapping materials. They are separate from the layers of the tarpaulin itself.

Read the unit or notation

This row is a material description, not a package dimension, packing weight or transport-protection rating. The original wording Craft paper is retained; confirm whether kraft paper is intended.

How it is measured or checked

Verify the agreed packing configuration and markings at dispatch. A material name alone does not define the strength, sealing or handling performance of the complete package.

Why it matters in use

Core dimensions, handling method and protection may matter for a converter’s equipment and transport arrangements. None is specified by the three packaging names alone.

Before comparing two sheets

Confirm core size, roll identification, packing arrangement and any pallet or handling requirements separately. Do not assume a pallet, waterproof transport guarantee or a particular gross weight.

15

MOQ

Example sheet · source wording3000yards for customization/ 100yards for in-stock

What this row means

MOQ means minimum order quantity. It is a commercial condition rather than a physical property. The source distinguishes customization from in-stock ordering.

Read the unit or notation

A yard is a length unit: 1yd=0.9144m. A square yard is an area unit. Confirm whether the table means linear yards, and which width, colour and version the quantity refers to.

How it is measured or checked

This row is checked against a current quotation and availability confirmation, not a laboratory test. If the unit is confirmed as linear yards, 100yd converts to 91.44m; that conversion is a unit example, not an updated sales offer.

Why it matters in use

Minimum quantities can affect sample planning, batch matching and production scheduling. The values on an example sheet should not be taken as proof of current stock or the current minimum for every requested variant.

Before comparing two sheets

Confirm the order unit, applicable configuration, present availability and current business terms with Duletai. Do not multiply the quantity into an area until the length basis and width are established.

Read more: NIST: unit-conversion factors

WHAT THIS SHEET DOES NOT LIST

A short sheet cannot answer every technical question. These are additional details to request if your project needs them; they are not extra measured values for DLT-5210.

  • Filament count, detailed yarn specification and weave
  • Density counting unit and notation order
  • Tolerances and typical/minimum value basis
  • Test methods, specimen directions and conditioning
  • Coating weight split, elongation, abrasion and water-pressure results
  • Welded-seam performance and detailed option-specific acceptance criteria

Do not fill these gaps using another model’s results. If the supplier adds them to an agreed specification later, keep their units, methods and conditions with the values.

FAQ

Does 1000D mean the finished tarpaulin weighs 1000gsm?

No. Denier describes yarn mass per length; gsm describes material mass per area. The finished material includes the reinforcement and coating layers.

Can I compare two 30×30 base fabrics directly?

First match the counting unit, fibre, yarn linear density and weave. The DLT-5210 example does not state the density unit or weave. Then compare finished-material test results under the same conditions.

Is a heavier or thicker fabric always stronger?

No. Area mass and thickness describe different aspects of construction. Read tensile, tear and relevant joint or adhesion results separately, with their test conditions.

Are all the options included in every roll?

An options list does not establish that. Confirm the selected construction and the written requirements for the offered material.

Why keep a missing unit or method visible?

Because adding an assumption changes what the original value means. Clarifying the missing information is more useful than comparing numbers on an invented basis.

PUT THE SHEET TO WORK

When contacting Duletai, describe the intended use, panel dimensions, converting process and the properties your project needs. Ask for the written specification for the exact offered material and clarify missing units or test conditions before comparing it with another sheet.

View the DLT-5210 example product · Discuss your fabric requirements

REFERENCES

The standards linked here explain measurement scopes. They do not establish that the example product was tested to them. Public catalogue pages and educational references were checked on 15 October 2026.

  • DLT-5210 source sheet
  • CottonWorks: yarn numbering
  • CottonWorks: basic woven designs
  • ISO 2286-1: roll length, width and net mass
  • ISO 2286-2: mass per unit area
  • ISO 2286-3: thickness at specified pressure
  • ISO 1421: tensile methods
  • ISO 4674-1: tear methods
  • ISO 2411: coating adhesion
  • NIST: unit-conversion factors
  • Duletai: PVC Tarpaulin Fire Standards
  • ISO 20743: antibacterial activity of textile products
  • ISO 22196: antibacterial testing scope and textile exclusion
  • ISO 846: effects of microorganisms on plastics

PVC Tarpaulin Fire Standards

  • 0
admin
Tuesday, 13 October 2026 / Published in Technology
Illustrative cargo-fire scene for PVC tarpaulin fire standards: Duletai presenter, burning tarp-covered goods, extinguisher responders and a regretful buyer. B1 on the label. Right test for the job?

Views: 244

Illustrative cargo-fire scene for PVC tarpaulin fire standards: Duletai presenter, burning tarp-covered goods, extinguisher responders and a regretful buyer. B1 on the label. Right test for the job?

Your supplier says the PVC tarpaulin is “B1”. Is that enough for your tent, membrane or awning project? Before you place the order, ask which standard that label refers to and whether the report covers the fabric you will actually receive. Flame-retardant PVC tarpaulin is made to limit burning under specified test conditions. It can still burn.

If you are comparing quotes, start with the project specification. Record the required standard and edition, the test method and the fabric construction, then compare those details with the supplier’s report. This guide explains what B1, M1 and NFPA 701 tell you, what they leave unanswered, and how the formulation affects cost and processing.

(more…)

Flame Retardant PVC Tarpaulin

  • 0
admin
Saturday, 07 June 2025 / Published in Technology

Views: 2682

Flame Retardant PVC Tarpaulin

Flame retardant PVC tarpaulin is a special type of polyester fabric combined with PVC​ and ​fire-resistant additives​. Unlike regular tarps, it slows down or stops fire from spreading, making it essential for places where fire safety is critical.When fire touches it:
✅ Slows down flames
✅ Stops burning when fire source is removed
✅ Protects what’s underneath

What’s Inside?​

Flame retardant PVC tarpaulin is manufactured through a specialized process that involves:

  1. Base Material: High-strength polyester canvas that provides structural integrity
  2. PVC: Coated or laminated polyvinyl chloride (PVC) layer 
  3. Flame Retardant Additives: Specific chemical compounds added during manufacturing
  4. Additional Additives: Accelerators, mildew inhibitors, anti-aging agents, and anti-static agents​
​Component​ ​What It Does​
Polyester Fabric Base Makes it strong and tear-proof
PVC Plastic Makes it waterproof & flexible
Fire-Stop Chemicals Prevents flames from spreading
Extra Protectors Fights UV rays, mold & aging
Core Technology and Materials
Antimony Trioxide (Sb₂O₃) Smoke Reduction​ Dripping Control​
Added to the PVC formulation to boost flame suppression. Reduce toxic fume generation by up to 50% during fire exposure. Reduced calcium carbonate formulation minimizes ​melt-dripping behavior.
Works with halogen compounds to form ​protective char barriers​ during combustion. Minimize release of hazardous chemicals (including HCl gas). Eliminates secondary fire hazards from falling molten material.
Significantly increases oxygen index (LOI) to achieve ​self-extinguishing properties. Create clearer evacuation pathways in emergency scenarios. Maintains fabric structural integrity at high temperatures.

️ ​Where it’s used?​

​Industry​ ​Applications​
​Transport​ Truck/train covers, cargo protection
​Construction​ Temporary shelters, scaffolding covers, debris containment
​Events​ Festival tents, stage backdrops, exhibition dividers
​Storage​ Warehouse covers, machinery protection
​Public Spaces​ Hospital barriers, school safety installations

​Global Safety Standards​

Standard Country/Region Key Classifications
Euroclasses (EN13501-1) European Union A1-F, s1-s3, d0-d2
M Classification France M0-M4
B Classification (DIN4102) Germany B1-B3
NFPA 701 United States Test Method 1 & 2
AS/NZS 1530 Australia/New Zealand Part 1-4
Key Tests:​ How fast fire spreads / How long it keeps burning / How much smoke it makes

Flame Retardant Levels and Requirements

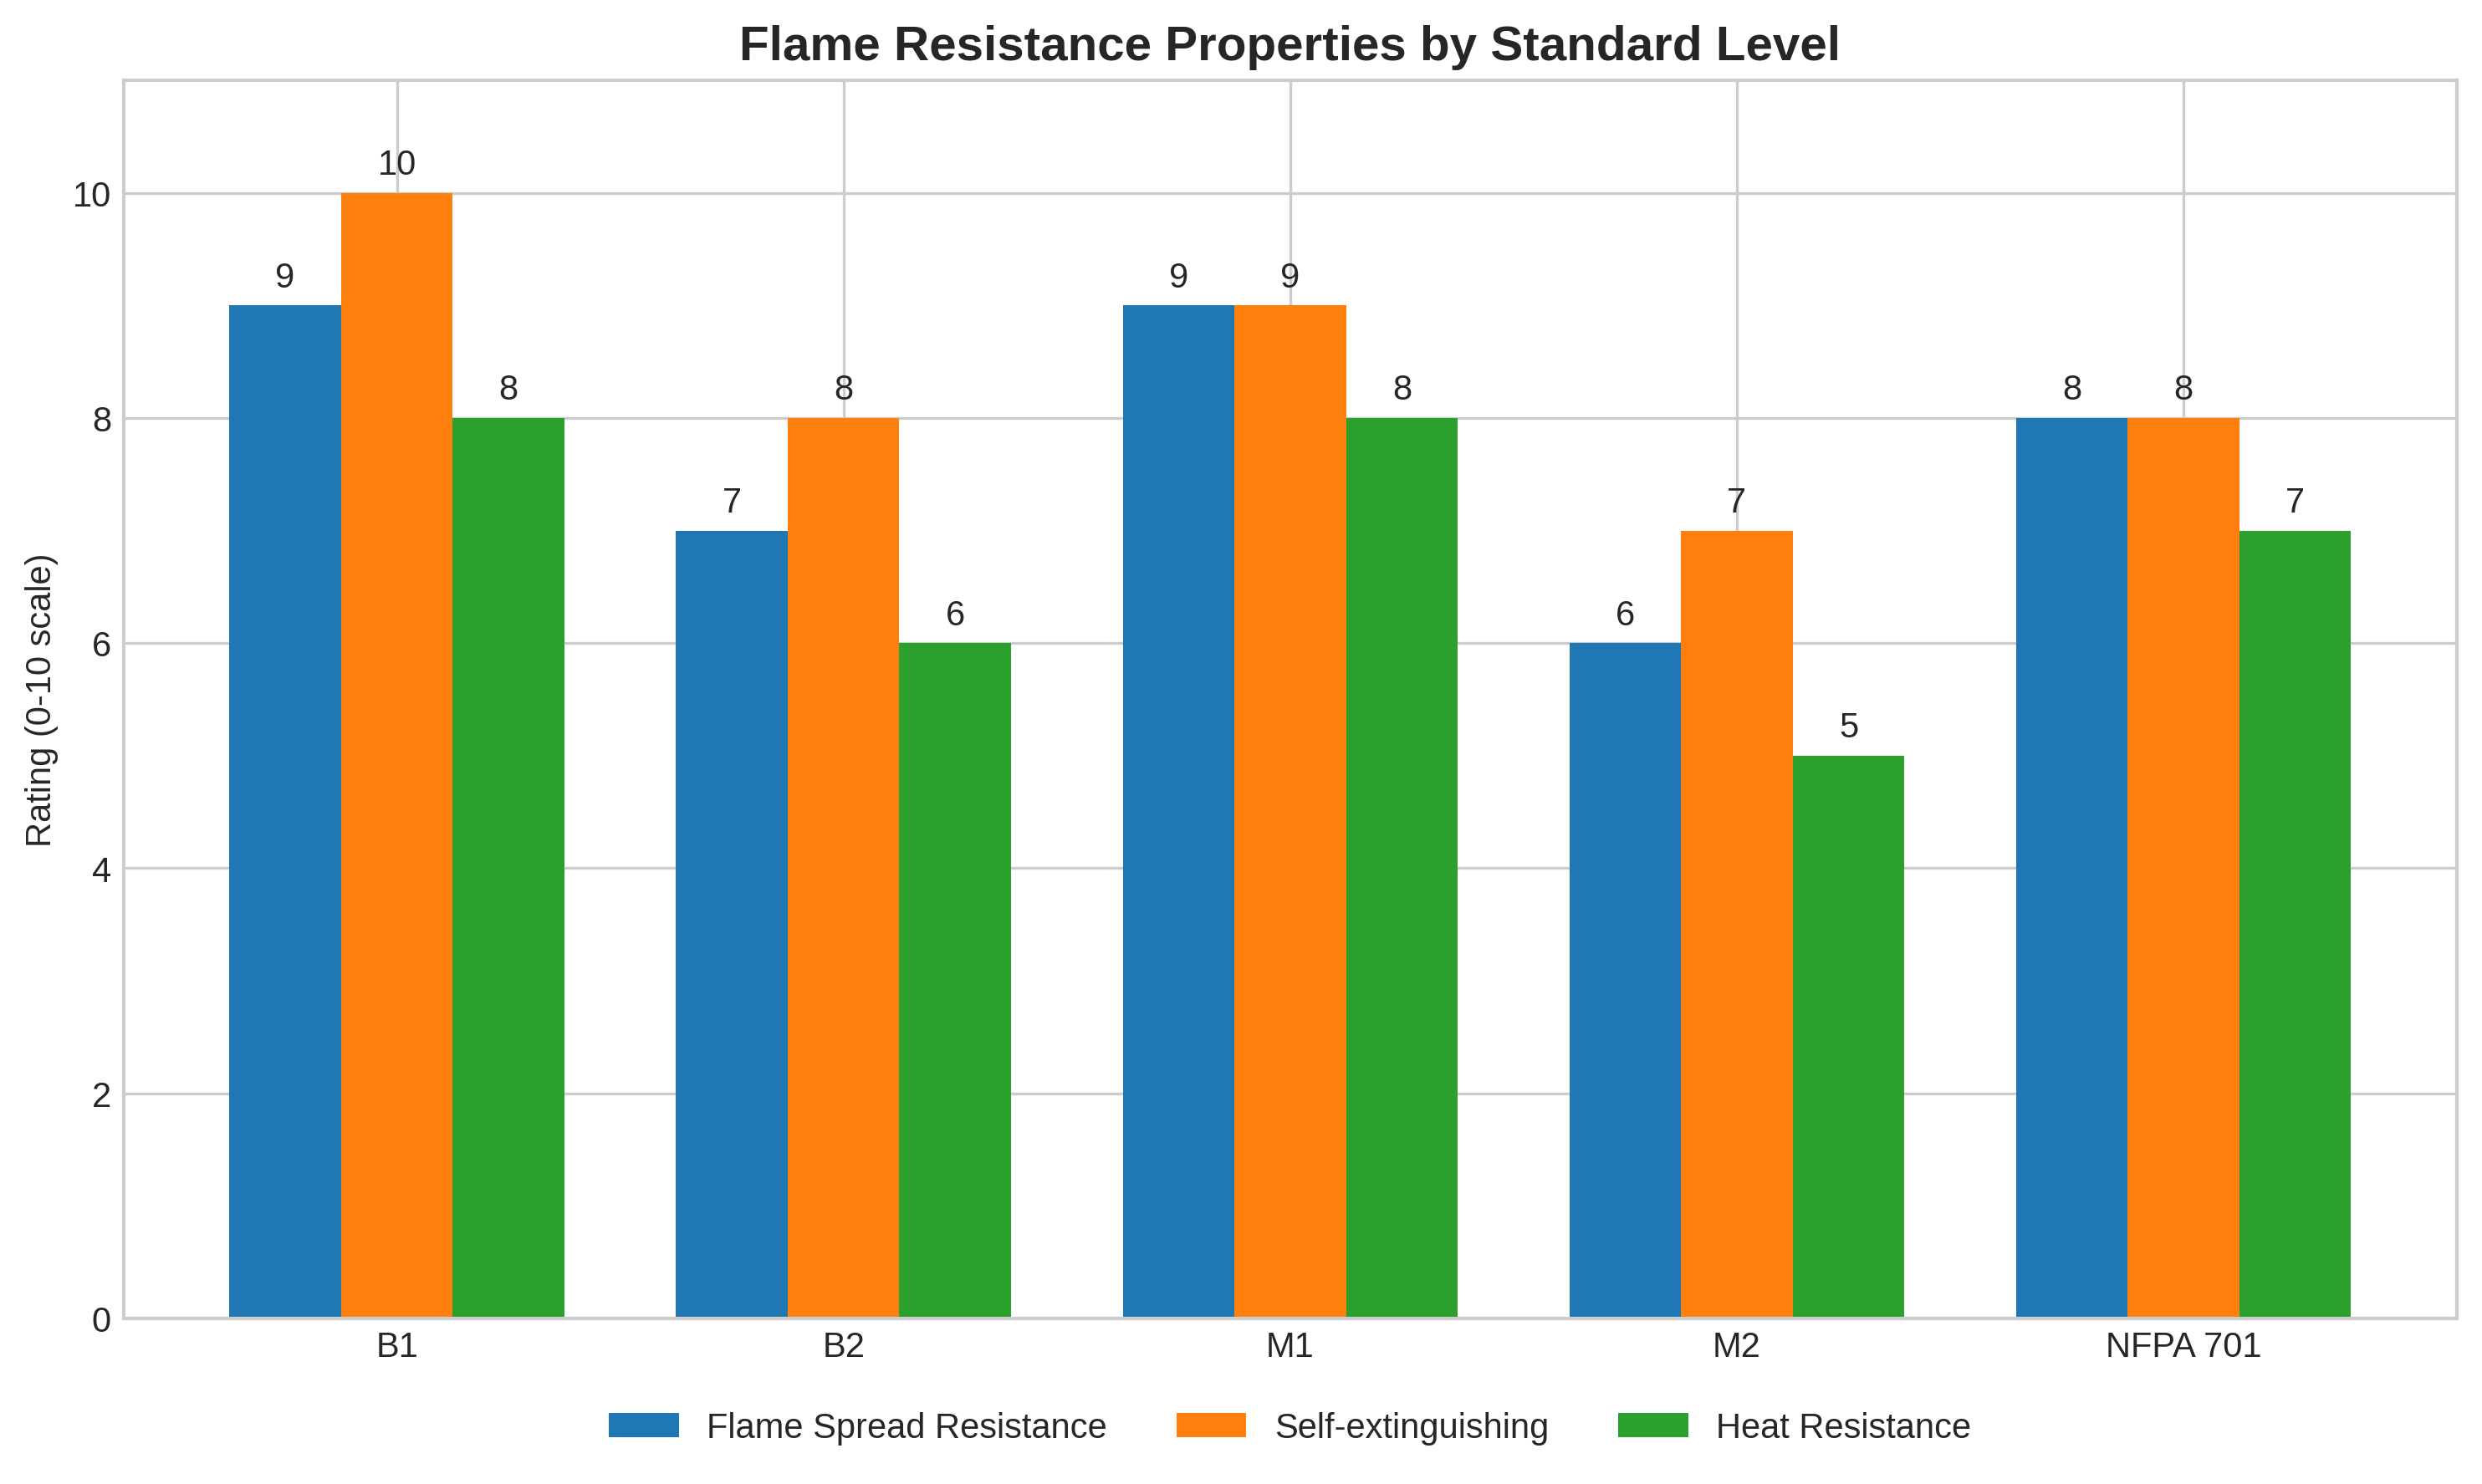
Level Description Requirements
B1 Fire retardant, self-extinguishing Difficult to ignite, limited flame spread
B2 Normally flammable, self-extinguishing Less fire resistant than B1
M1 Non-flammable combustible materials Excellent fire resistance, low flammability
M2 Flammable materials with low flammability Medium fire resistance
NFPA 701 Test 1 For materials ≤700g/m², single-layer fabrics Pass flame propagation test
NFPA 701 Test 2 For plastic films, vinyl-coated fabrics Pass flame propagation test for heavier materials

Flame Retardant PVC Tarpaulin

Choosing Your Protection Level​

​Fire Danger Level​ ​Best Standard​ ​Good For…​​
High risk B1 or NFPA 701 Method 2 Welding areas, chemical storage
Medium risk NFPA 701 Method 1 Event tents, truck covers
Basic protection General flame retardant Temporary covers, indoor use

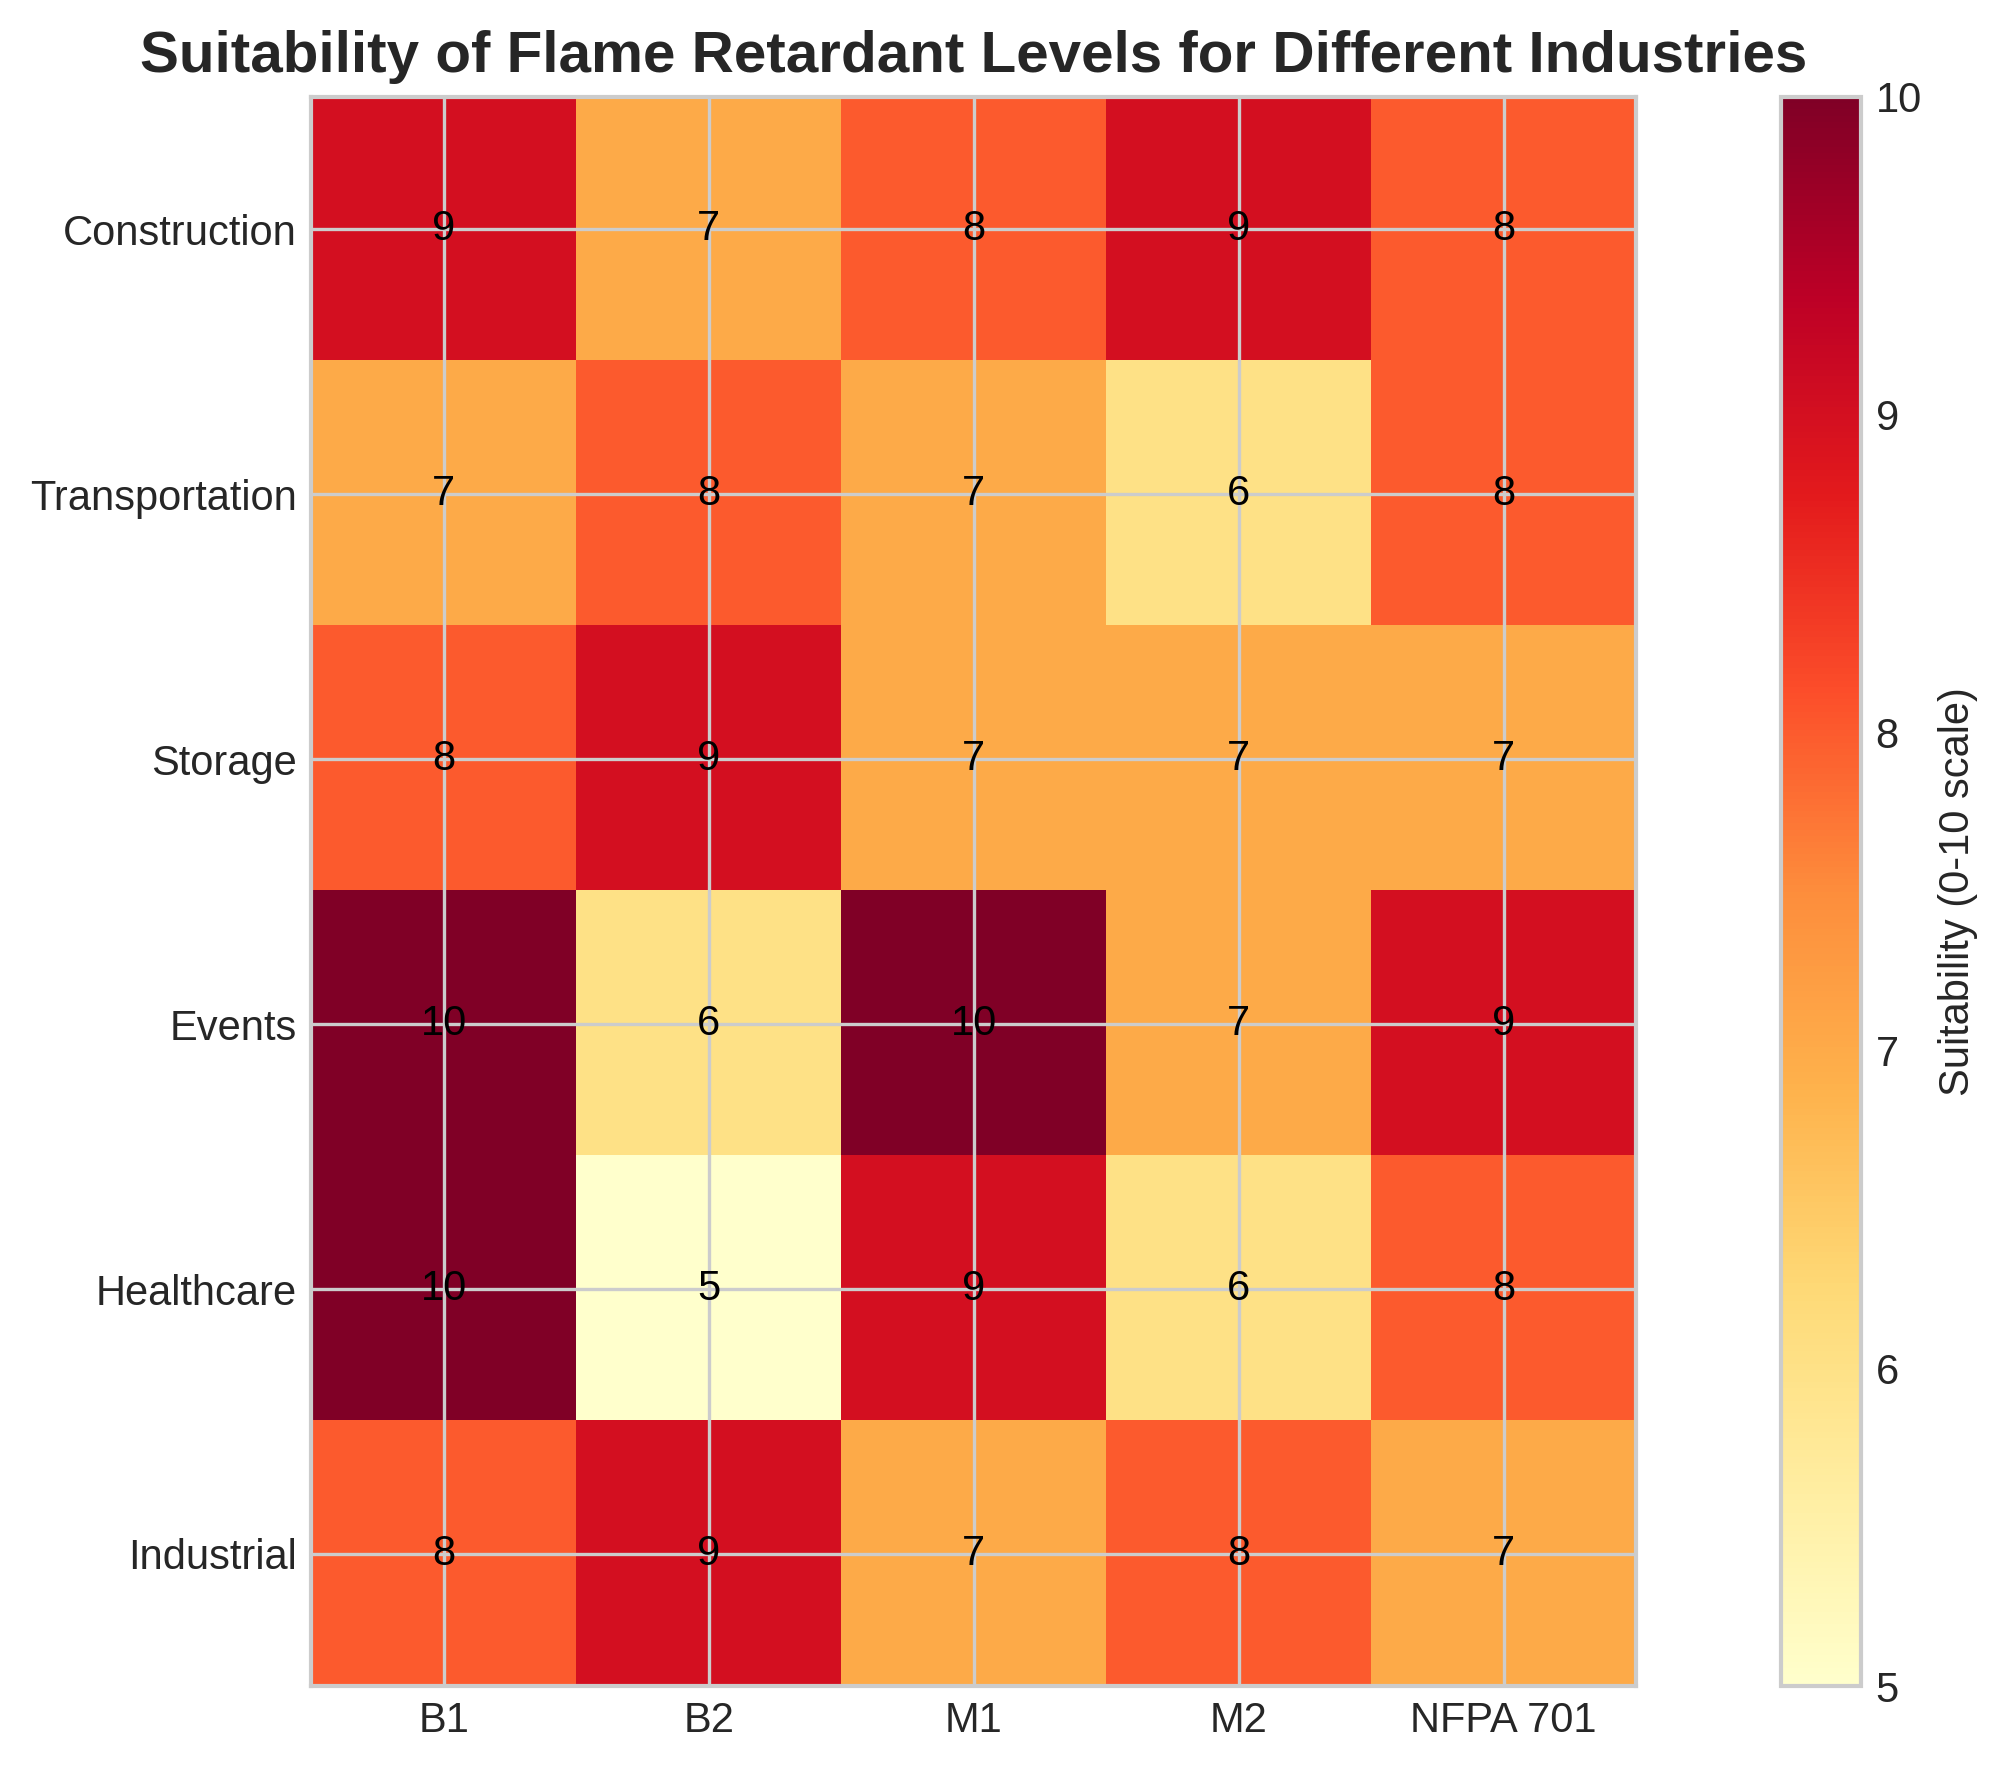
Applications of Different Flame Retardant Level Materials

Level Common Applications Industry Sectors
B1 Public buildings, exhibition halls, theaters, hospitals Construction, Events, Healthcare
B2 General industrial use, warehouses, temporary structures Industrial, Storage, Transportation
M1 Public buildings, high-risk environments, theaters Events, Entertainment, Public facilities
M2 Commercial buildings, standard requirements Commercial, Industrial
NFPA 701 Commercial buildings, public spaces in the US Commercial, Public facilities, Events

Flame Retardant PVC Tarpaulin


What is vinyl tarpaulin material?

  • 0
admin
Tuesday, 21 March 2023 / Published in Technology

Views: 1509

Vinyl tarpaulin material is a highly durable and versatile material that is widely used in a variety of applications. It is made from polyvinyl chloride (PVC) and is often referred to as PVC tarpaulin. This material is known for its excellent resistance to water, UV rays, and mildew, making it ideal for use in outdoor applications.

Vinyl tarpaulin material is commonly used as a cover for boats, trailers, and trucks. It is also used in the construction industry for scaffolding, as a temporary shelter, and to cover building materials. Additionally, it is used as a tent material for outdoor events and camping trips.

vinyl tarpaulin material

One of the main advantages of vinyl tarpaulin material is its strength and durability. It is resistant to punctures, tears, and abrasions, which makes it ideal for use in harsh environments. Additionally, it is flexible and easy to handle, making it easy to install and transport.

Vinyl tarpaulin material is available in a variety of colors and thicknesses to suit specific needs. It can be made to be opaque, translucent, or transparent, depending on the application. It is also available in flame-retardant varieties, making it ideal for use in applications that require fire resistance.

Another advantage of vinyl tarpaulin material is its affordability. It is a cost-effective alternative to other materials such as canvas, which can be more expensive. Additionally, it requires very little maintenance and can be easily cleaned with soap and water.

However, there are some disadvantages to using vinyl tarpaulin material. One of the main disadvantages is that it is not environmentally friendly. PVC is a plastic material that is not biodegradable and can release harmful chemicals when it is burned. Additionally, it can be difficult to dispose of properly, which can lead to environmental pollution.

In conclusion, vinyl tarpaulin material is a durable and versatile material that is widely used in various applications. It is affordable, easy to handle, and resistant to water, UV rays, and mildew. However, it is not environmentally friendly, and its use should be limited to applications where other materials are not suitable.

Everything You Need to Know About Outdoor Fabrics

  • 0
admin
Thursday, 09 September 2021 / Published in Technology

Views: 1680

Today’s outdoor fabrics are nothing like the outdoor fabrics of old. Outdoor fabrics have come a long way since barkcloth, oilcloth, and vinyl. We now have a multitude of outdoor fabrics made from superior materials, such as 100% solution-dyed acrylic and 100% high UV-resistant polyester. Not only are there better outdoor fabric materials, but there is also a variety of outdoor fabric styles to perfectly coordinate with your décor, including bright colors, stunning patterns, and intricate textures.

Can I Use Indoor Fabric Outdoors?

Sure, but don’t expect your cushions and pillows to last long! Indoor fabric colors bleed when wet and fade easily. Unlike many indoor fabrics, outdoor fabrics are designed with longevity in mind. Outdoor fabrics are made to withstand UV rays, precipitation, pollen, dirt, and mildew. They are easily cleaned by simply brushing off dirt or by using a solution of mild soap and water.

Can I Use Outdoor Fabric Indoors?

Yes! In fact, in many situations, outdoor fabric is probably best. Because it’s stain- and water-repellent as well as easy to clean, outdoor fabric is an excellent option for homes with children, pets, and high-traffic areas. And because outdoor fabric is tough against fading, it is great for furniture situated near windows. If you are thinking that outdoor fabrics are scratchy and stiff, that’s no longer the case. Many of today’s outdoor fabrics feature soft textured weaves and jacquards.

Is There a Difference Between Outdoor Fabric Brands?

Yes. Not all outdoor fabrics are created equally. While the majority of the outdoor fabrics produced today are made of synthetic materials, each brand uses a different manufacturing process or provides a different textile blend. Some of the most popular outdoor fabric types include 100% solution-dyed acrylic and 100% high UV polyester. Because these fabrics are made of synthetic fibers, they are both mildew- and mold-resistant. Each fabric brand carries different warranties on fading. Brands with fabric made from 100% solution-dyed acrylic carry warranties ranging from 5-6 years while brands featuring 100% high UV polyester have a 3-year warranty.

Sunbrella Fabrics
Outdoor Fabric
One of the most well-known outdoor fabric brands is Sunbrella, which is made with 100% solution-dyed acrylic yarns. However, other brands, like Outdura, PARA` Tempotest, and Robert Allen Open Air are also made of the same type of material. The manufacturing process of these fabrics is what makes these brands so exceptional. During the solution-dyed acrylic yarn making process, color is added to the acrylic fibers while they are still in a liquid state, giving the fabrics long-lasting color. . Also during production, the fabric is treated with a stain- and water-repellent finish. 303 Fabric Guard replaces this finish if it has been removed after cleaning.

Al Fresco Fabrics
Al Fresco Functional Fabrics are made from 100% high UV-resistant polyester. Unlike many polyester outdoor fabrics, Al Fresco fabrics are not screen printed. Instead, the yarns are woven, creating a lasting design with a higher resistance to fading. Although 100% solution-dyed acrylic fabrics have a better warranty against fading, some Al Fresco fabrics, like the Cabana Stripes and Denims, pass an impressive 117,000 double rubs.

Which Outdoor Fabric Should I Choose?

Choosing the right outdoor fabric depends on how you plan to use it. Solution-dyed acrylic and woven polyester work well for all indoor and outdoor throw pillows and drapes. For cushions, upholstery, or other frequently used items, 100% solution-dyed acrylic and Al Fresco’s fabric that passes 117,000 double rubs are best. Anything that will spend extensive hours in the sun should be made with 100% solution-dyed acrylic because of its high UV rating.

Overall, the best fabric is the one you love most. Now that there is a wealth of options, it is easier to find a favorite fabric that is suitable for outdoors.

Introductions of Outdoor Fabrics

  • 0
admin
Thursday, 05 August 2021 / Published in Technology

Views: 1117

Outdoor fabrics differ from indoor fabrics in that they are made to be more durable, and they undergo a chemical treatment process during manufacturing that ensures they will resist stains and mildew. Outdoor fabrics are woven fibers that differ in strength and durability. The primary difference between each type of the most commonly used outdoor fabric lies in the manufacturing process and the fibers that they are made from.

outdoor fabrics

Solution-Dyed Acrylics

Solution-dyed acrylics are fabrics that are dyed before the yarn is created. Most fabrics begin colorless, and then the fibers are woven into yarn, and the yarn is dyed before it is woven into a fabric. With solution-dyed acrylic, a liquid acrylic solution is mixed with the dye, and then it is formed into a fiber so it already has color before it is spun into a yarn. This process makes it color-fast and water-resistant. Solution-dyed acrylics are soft and breathable like canvas and are commonly used in awnings and patio umbrellas, but a softer, more porous version is also used for outdoor pillows and cushions.

acrylic awing fabric

Acrylic-Coated Polyesters

Acrylic is used as a base for many outdoor fabrics because of its durability and resistance to wrinkling, fading, and mildew growth. Polyester shares may of these properties, and the use of both fabrics in one material makes a durable outdoor fabric. To make acrylic-coated polyester, the fabric threads are woven first and then the material is dipped into an acrylic coating to color it. This fabric is also available in cotton-polyester blends, which typically have a more appealing appearance. Acrylic-coated polyester and cotton-polyester blends are typically used to make boat and car protectors but may also be used as patio umbrellas and awnings.

Camouflage oxford fabric


Vinyl-Coated Synthetic Fiber Mesh

Vinyl-coated synthetic fiber mesh is also referred to as PVC mesh or slingable fabric. It is often used for sling-type outdoor chairs, whose fabric — not the frame — supports your weight. This fabric is strong and does not stretch. Other fabrics, such as solution-dyed acrylic, printed polyester and printed acrylic outdoor fabrics, are not strong enough to cover these types of chairs. Most PVC mesh fabrics are made of vinyl-coated polyester or acrylic yarns, as well as other synthetics such as olefin and PVC, but the composition of materials varies depending on the manufacturer. They make a durable, easy-to-clean, colorfast and strong outdoor fabric that doesn’t promote mildew growth.

sunscreen fabrics

Olefin

Olefin is a manmade fiber that is typically used along with other fibers to create outdoor fabric blends. It is often used in outdoor furniture and for a variety of other applications, including house wrap, marine coverings and clothing. Depending on its chemical structure, olefin may also be referred to as polyethylene or polypropylene. It is manufactured in a similar manner as polyester and nylon. The chemicals used are melted and fed through a shower-head-like device called a spinneret head to form long fibers. Olefin typically has a smooth texture and is usually solution-dyed. It is a durable fabric that dries quickly and resistant to weathering, chemicals, stains and mildew.

Olefin outdoor fabric

Canvas

Canvas is a strong, heavy-duty outdoor fabric used to make sails, tents, backpacks, tarps and even canoes. Modern canvas fabrics may be made from a variety of materials but are usually made using cotton or linen. Canvas is also a generic terms used to describe a variety of outdoor fabrics, including polyester, acrylics and blends of these materials. Mold and mildew are a major drawback of cotton or linen-based canvas fabrics because many true canvas materials are made of natural fibers.Outdoor fabrics

About Different Roller Blinds Applications

  • 0
admin
Friday, 23 July 2021 / Published in Technology

Views: 783

Roller blinds are a popular choice amongst homeowners, favoured for their attractive and fresh design. They are very versatile and can suit and enhance any type of interior décor. Roller blinds are also very functional when it comes to controlling (or blocking out) light, providing privacy and good insulation.

Roller blinds come in many different designs and materials, so there’s plenty of choice when it comes to styling your home!

Some of the most popular styles include:

  • Blockout roller blinds
  • Light filtering roller blinds
  • Sunscreen roller blinds

These designs are all available in different colours and materials. They also have wonderful UV ratings to protect furnishings in your house.

Rooms Where Blockout Roller Blinds Are Most Often Used

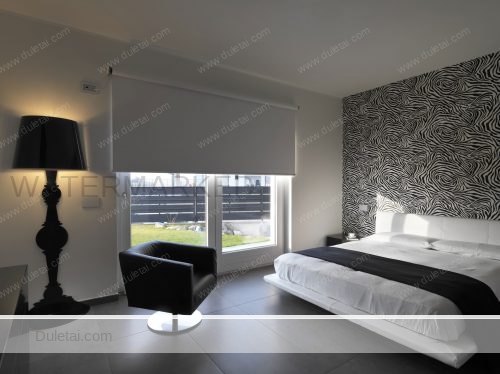
 Bedrooms

Blockout roller blinds are perfect when installed in bedrooms. Blockout fabrics are very good at offering privacy and blocking out unwanted light during the day or night. When the blinds are rolled down, you can enjoy high levels of privacy in your bedroom.

Roller Blinds Applications


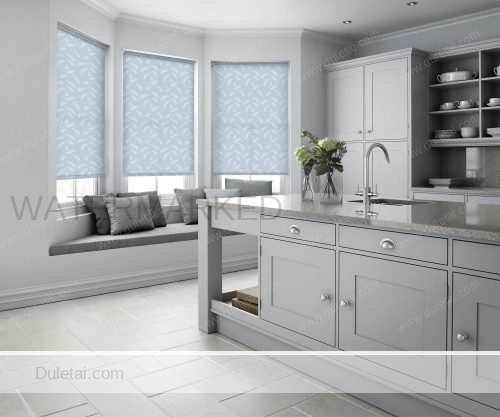
Kitchens

Blockout and sunscreen fabrics are the two most preferred types for kitchen window blinds. Which of the two you choose comes down to your desired level of privacy. Using water-resistant materials for kitchen windows is also a good idea to prevent damage and unsightly stains.

Roller Blinds Applications

 Living Rooms

Most homeowners use all three types of roller fabrics together in their living areas. In fact, they may use combination brackets and install dual roller blinds to allow the use of any roller at any time. The sunscreen option is usually used during the day when the sun is shining, while the blockout roller option is used at night when darkness sets in.

Roller Blinds Applications

 Offices

Office spaces usually have sunscreen roller blinds installed on their windows. This is because they are effective at reducing sun glare, light and heat during the day. Blockout roller blinds can also be installed in conference rooms where light reduction may be necessary.

Roller Blinds Applications

 Bathrooms

These rooms require a high level of privacy, so blockout materials are the most common choice. When choosing materials for a bathroom, consider choosing a water-resistant material. Light filtering rollers could also be ideal because they offer both light and privacy.

Which fabric is best for a projector screen?

  • 0
admin
Monday, 26 April 2021 / Published in Technology
projection screen fabric

Views: 8629

When you’re looking to purchase a new projector screen, then there are some things that you’ll want to think about first. Getting the right size screen is important, as well as the method it uses to stand up or retract. But, you should also consider what fabric and material the screen is made out of.

If you want a truly good experience with your projector, then using the right screen fabric with it is essential. But what is the best fabric to use for a screen projector? Well, we’re going to look at some of the fabrics that you can use with a projector screen to give the best experience.

Which fabric is best for a projector screen?

If you’re looking for the best fabric for a projector screen, then the right answer is to use a white blackout cloth. You can pick this up for a very reasonable price, and you can can even choose to paint your blackout cloth to create an even better experience.

You can usually pick up this kind of blackout cloth online, or from your local hardware store. Getting the right cloth is important for your picture quality. Plus, if you make it yourself, you’ll need to put in some effort to get the right aspect ratio.

Though I think it’s the best, this isn’t the only material that you can use as a projector screen. So, let’s look at some of the best options out there so you can find the right one to suit you.

Blackout Cloth

If you’ve ever worked the night shift, then you’ll know what material I’m referring to here. It’s the same material used for blackout curtains, and it’s designed to specifically keep out light – it’s made from cotton and polyester. It also works really well as a projector screen, as it’s non reflective and it can be viewed from any angle.

As I also mentioned, you can actually choose to add some paint to your blackout cloth to give it an even better appearance. Whilst you could do this with a roller, it’s probably a better idea to use some spray paint on the cloth. You also might want to use some primer too, which should give you an even better finish.

If you’re looking to make your own projector screen, then this isn the best material to use. However, there are other options out there too that can work as a makeshift fabric for your projector. One good idea is to use roller blinds, which can make for a good projector screen material.

Paint/Wall

Although the majority of the time you’re going to want to use a sort of fabric as your screen, there’s also another alternative which has no fabric at all. I’m talking about using paint as the screen itself, as you can get specially made paint that’s designed specifically for projecting images onto it.

The colour that you use for the paint is going to be important. Most people tend to opt for a white colour as you’d expect. You can also look at going for a black or grey colour too, and it will all depend on the time and ambience of the room when you’re going to use the projector.

You’ll also have to consider the style of the paint you’re using as well. If you use matte paint, then the picture can be a little dark and there will be no vibrancy in the image. On the other hand, if you use glossy paint, then it is going to be too reflective.

From a negative perspective, with a wall you’re not going to have complete control over how smooth the surface is. A screen is very smooth, but your wall may have little bumps and nicks in it that may effect the quality of your viewing.

Other Options

These are the best options for those looking for a DIY solution. But, there are other materials out there you can use, and that are used by larger companies making screens professionally. Here are a few of them.

Plastic – A common surface for a screen can just be ordinary plastic. This is because the material use as the surface isn’t as important as the coating on the display itself. This is one of the most cost effective solutions.
Metal – Although nowhere near as common, another material that is used for projector screens is metal. This is mainly with low lumen projectors, and not those made for commercial use.
Fibreglass – For those looking for an increase in quality in comparison to plastic, then you can also find screens that are made of fibreglass. They’re a good choice if you want something that will last.
PVC – You will also find projector screens out there made from PVC. However, they’re nowhere near as common as plastic projector screens.

Conclusion

In conclusion, the best option if you’re looking for a good material to use as a projector screen is a type of blackout cloth. This fabric isn’t particularly expensive, and can easily be used to create a DIY projector screen.

The thing is with DIY screens is that they can take a little while to make, and if you’re not entirely sure on the colour screen you need, this can make it even more difficult.

Of course, you could also avoid creating your own DIY screen and opt to purchase one ready made. Nowadays, screens are more reasonably priced than ever, and you might even be able to get one for not much more than it would cost to do it yourself.

What is the difference between Laminate & PVC coated material?

  • 0
admin
Wednesday, 07 April 2021 / Published in Technology

Views: 2701

The main difference between laminates and PVC coated material is in how the components are held together. Laminate material is held together by fusing or rolling a top and bottom material around the base cloth, simply fusing the laminate coating layers to each other through the open spaces of the base cloth. PVC coating, however, is bonded to the base fabric by using a special adhesive process.The first step in this process is to spread a high strength adhesive in and around each base cloth thread. Then the PVC coated material, which is in a liquid state, is spread over the glue. Finally they are all fused together using heat and pressure.

When you polled most professionals in the tent rental industry, the majority answer would be cost. As it turns out, cost is only a result of the overall equation that is too often the ending point for many conversations on the subject. The primary difference in these fabrics rests in the method of the application of the vinyl to the base fabric. The results of these two construction methods each have their own benefits and drawbacks.
pvc coated material

Laminated PVC is composed of a base polyester scrim that is placed between two or more layers of PVC film. These multiple layers of material in huge roll form are fused together in a PVC Laminating machine using extreme pressure and heat to create one solid piece of fabric. Often opaque layers and adhesives are additionally used to attain desired specifications. The formed material is passed over rollers to create the desired finished appearance (i.e. glossy, matte, etc.). The thickness of the raw PVC film on each side of the scrim added to the base fabric (scrim) result in a desired finished weight can add to its performance under Ultraviolet (UV) conditions (on the top side of the laminate) and abrasion resistance (on the bottom side of the laminate).

As a result of the application of a consistent layer/thickness of film on each side of the fabric, the film will fill into the hills and valleys of the base fabric creating a rougher texture (usually on the back side of the fabric). The narrower the openings of the mesh (base fabric) causes a reduction in the depth of the hills and valleys to fill and result a smoother the final appearance of the finished product. Unfortunately, the narrower the openings in the base fabric will in turn decrease the adhesion of the film to itself resulting in “delamination” or poor welding performance. Increasing the thickness of the PVC film will also result in a smoother product but will also add more weight to the finished fabric

Most all vinyl used in the construction of tents is inherently flame retardant, meaning that no additional flame retardant treatment is ever necessary during the lifetime of the fabric. Laminated fabrics are commonly used in the following weights: 12oz/sqyd, 16oz/sqyd, 18oz/sqyd and can be fabricated in any range from 10oz to 28oz.

PVC coated material is composed of a similar base polyester fabric that is passed through molten liquid vinyl and then extruded (or shaved) down to the desired thickness. As with laminated fabrics the coated formed material is passed over rollers to create the desired finished appearance. The resulting fabric is generally smoother on both sides when compared to laminate PVC. The thickness of the raw PVC film on each side of the scrim added to the base fabric (scrim) result in a desired finished weight can add to its performance under Ultraviolet (UW) conditions (on the top side of the laminate) and abrasion resistance (on the bottom side of the fabric).

The result of the extrusion or shaving of the PVC to the base fabric creates a PVC layer that is contoured to the base fabric, filling the valleys with PVC while the exposed surface remains very smooth.

Most all vinyl used in the construction of tents is inherently flame retardant meaning that no additional treatment is ever necessary during the lifetime of the fabric. PVC coated material are commonly used in the following weights: 18oz/sqyd, 20oz/sqyd, 24oz/sqyd and can be fabricated in any range from 16oz/sqyd to 32oz/sqyd.

Benefits & Draw Backs:

Laminated Fabrics:
Benefits
• Lower cost
• Greater availability (Domestic Production)
• Greater color selection
• Less stringent parameters for special order runs (often around 500yd minimums)
• Higher strength to weight ratio-Both tensile and tear strengths
• Most domestic patterning is based on 61” width goods (all manufacturers)

Drawbacks
• Rougher under side of fabric, less easy to clean
• Less resistance to pin holes (as a result of less PVC in the fabric)
• Less pliable with age (as a result of less PVC in the fabric)

Coated Fabrics:
Benefits
• Smoother finish (easier to clean)
• High tensile strength
• Greater durability
• Greater resistance to pinholes
• More pliable in cold weather conditions

Drawbacks:
• Higher cost – (weak Dollar, transportation, lead time, etc.)
• No domestic production
• Stringent parameters for special order runs (often around 5500yd minimums)
• Very few color options
• Fewer weights to choose from
• Weaker tear strength

  • 1
  • 2
  • 3
  • 4

Categories

  • News
  • Technology

Latest posts

  • PVC fabric cross-section distinguishing the intact surface barrier from water movement along exposed reinforcement

    PVC Surface Finishes & Anti-Wicking

    Understand PVC finishes, anti-wicking and knife...
  • PVC Tarpaulin Datasheets Explained

    Learn how to read a PVC tarpaulin datasheet, fr...
  • Illustrative cargo-fire scene for PVC tarpaulin fire standards: Duletai presenter, burning tarp-covered goods, extinguisher responders and a regretful buyer. B1 on the label. Right test for the job?

    PVC Tarpaulin Fire Standards

    A practical guide to PVC tarpaulin flame retard...
  • Flame Retardant PVC Tarpaulin

    Views: 2682 Flame retardant PVC tarpaulin is a ...
  • Weather-Resistant PVC Knife-Coated Tarps

    Views: 1697Weather-resistant PVC knife-coated t...

MAIN SITE

  • Duletai.com

SUB SITES

  • DuraInflate.com

SALES OFFICE / SHOW ROOM

Tel:+86-133-96832665
Email: Sales@duletai.com

NO.23 Wenli Road, Haining, Zhejiang, China Postal code: 314400

FACTORY

Tel&Fax:+86-573-87798816
Email: Duletai@outlook.com

NO.25, Hongqi Road, Haining, Zhejiang, China Postal code: 314400

Duletai New Material

2020©Haining Duletai New Material Co.,Ltd. All rights reserved.

TOP